

End Milling 101: A Beginner’s Overview
End milling is one of the most versatile machining processes used in modern manufacturing. From precision grooves and pockets to complex contours, it allows manufacturers to create a wide range of features on metal and other engineering materials.
End milling uses rotating cutting tools called end mills to remove material from a workpiece. Depending on their design, end mills can cut with their end and peripheral edges, making them suitable for slotting, profiling, pocket milling, and finishing operations.
End milling is widely used in aerospace, automotive manufacturing, mold making, and general mechanical engineering. However, achieving accurate results requires choosing the right end mill, cutting parameters, and machining strategy.
This beginner's guide explains what end milling is, the main types of end mills, their applications, and how to use them effectively.
I. What Is End Milling?
End milling is a machining process that uses a rotating end mill to remove material from a workpiece.
Unlike cutting methods that primarily produce flat surfaces, end milling can machine various features, including slots, pockets, shoulders, and complex profiles.
An end mill typically has cutting edges along its sides and at its end, allowing it to remove material through peripheral cutting, end cutting, or a combination of both.
This flexibility makes end milling an important operation on CNC milling machines and machining centers.
II. What Is an End Mill?
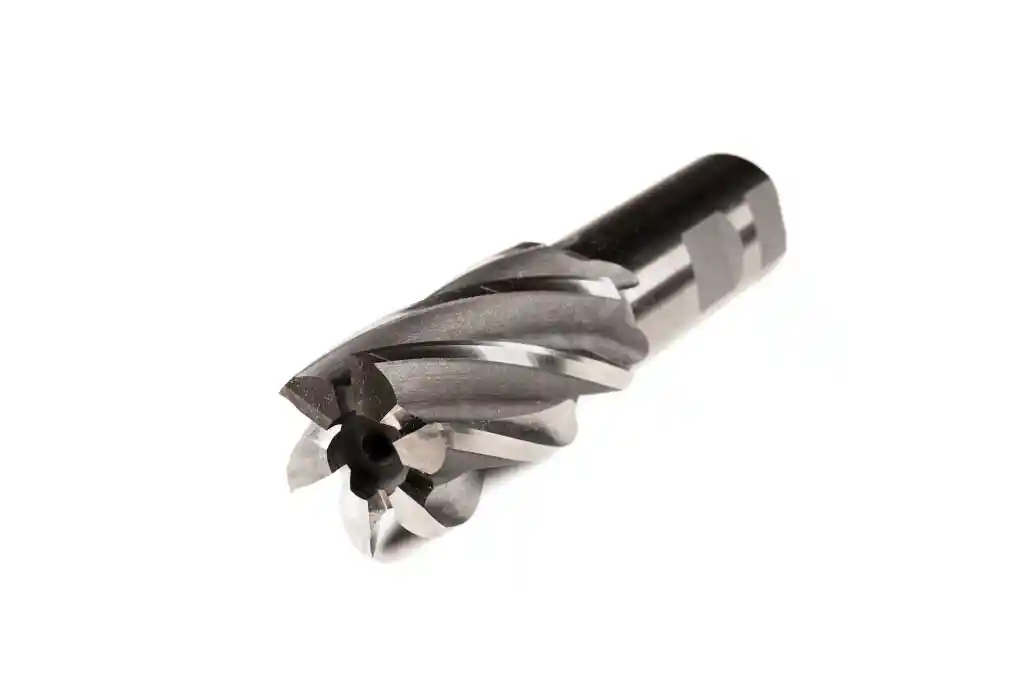
An end mill is a rotating, multi-edge cutting tool designed for milling operations.
Most end mills have cutting edges along the cylindrical surface and at the tool end. Their geometry determines which operations they can perform effectively.
End mills are commonly used to machine:
- Flat surfaces and shoulders
- Slots and grooves
- Pockets and cavities
- External and internal contours
- Complex three-dimensional surfaces
Different end mill designs are available for roughing, finishing, and specialized machining tasks.
Not all end mills can plunge directly into solid material. Center-cutting capability, tool geometry, and the recommended entry method must be considered when selecting a cutter.
III. When Should You Use End Milling?
End milling is commonly performed on CNC milling machines and machining centers. It is particularly useful when a component requires more than simple flat-surface machining.
Typical applications include:
Slot Milling: Creating grooves, channels, and suitable keyways in mechanical components.
Pocket Milling: Removing material from enclosed or partially enclosed areas to produce cavities and recesses.
Shoulder Milling: Machining steps and surfaces that meet at defined angles, often 90 degrees.
Profile Milling: Producing external contours, internal profiles, and complex shapes.
Surface Finishing: Improving the dimensional accuracy and surface quality of suitable machined features.
End milling is useful for prototype development, small-batch machining, and repeat production.
For example, a CNC machining center may use a square end mill to create a pocket in an aluminum housing and a ball nose end mill to finish a curved mold surface.
The choice of end milling operation depends on the workpiece geometry, material, required accuracy, and surface finish.
IV. Types of End Mills and How to Choose Them
End mills are available in different shapes, flute configurations, and tool materials.
Choosing the correct type is important for machining efficiency, surface quality, and tool life.
Shapes of End Mills
Square End Mills
Square end mills have a generally flat cutting end and are commonly used for slotting, pocket milling, shoulder milling, and machining flat-bottomed features.
They are among the most widely used end mills in general CNC machining.
Ball Nose End Mills
Ball nose end mills have a rounded cutting end, making them suitable for machining curved surfaces and three-dimensional contours.
They are frequently used in mold making and other applications requiring complex surface finishing.
Corner Radius End Mills
Corner radius end mills have a small radius at the intersection of the end and peripheral cutting edges.
This geometry can improve edge strength and reduce corner chipping under suitable cutting conditions.
They are used for both roughing and finishing operations.
Roughing End Mills
Roughing end mills often feature serrated or specially designed cutting edges that divide chips into smaller segments.
They are used for efficient material removal before finishing operations.
Specialty Cutters
V-bit cutters are commonly used for engraving and V-shaped grooves, while corner-rounding cutters create rounded edges.
Fishtail cutters may be used in certain routing and specialized cutting applications, depending on their geometry.
For dovetail slots, a dedicated dovetail cutter is generally required.
These specialized tools should be selected according to the intended feature rather than treated as interchangeable with standard end mills.
Number of Flutes
Flutes are the grooves along an end mill that provide cutting edges and space for chip evacuation.
The number of flutes influences chip removal, cutting stability, and suitable feed rates.
2-Flute End Mills
Two-flute tools provide relatively large spaces for chip evacuation.
They are commonly used for aluminum and other materials that produce substantial chips, particularly in slotting operations.
3-Flute End Mills
Three-flute end mills offer a balance between cutting-edge engagement and chip clearance.
They are commonly used for aluminum machining and can be suitable for selected roughing and finishing operations.
4-Flute End Mills
Four-flute end mills are widely used for steel and other suitable materials.
They provide additional cutting edges and can support efficient machining when chip evacuation and cutting conditions are properly managed.
Flute count should not be selected based on material hardness alone. The machining operation, chip volume, tool geometry, and manufacturer's recommendations are equally important.
Materials Used for End Mills
The cutting tool material influences wear resistance, toughness, cutting speed, and cost.
High-Speed Steel (HSS) End Mills
HSS tools are relatively economical and offer good toughness.
They can be suitable for lower-speed machining and general-purpose applications.
Cobalt HSS End Mills
Cobalt-alloyed high-speed steel offers improved hot hardness compared with many conventional HSS grades.
It can be useful for selected machining applications requiring better heat resistance.
Carbide End Mills
Solid carbide end mills generally provide high hardness, wear resistance, and rigidity.
They are commonly used for high-performance CNC milling, particularly when higher cutting speeds and precise tool geometry are required.
However, carbide is less tolerant of impact and excessive vibration than tougher tool materials, so machine rigidity and secure workholding are important.
For beginners, the best end mill is not necessarily the most expensive one. It is the tool that matches the workpiece material, machining operation, machine capability, and required results.
V. Applications of End Milling
End milling is used across multiple manufacturing industries because it can produce both simple and complex machined features.
Aerospace Manufacturing
End milling is used to machine pockets, profiles, and structural features in suitable aerospace components.
For example, aluminum structural parts may require lightweight pockets and accurate contours.
Automotive Manufacturing
CNC end milling is used for housings, brackets, engine-related components, and transmission parts.
Common operations include pocket milling, shoulder milling, and precision profiling.
Mold Making
Ball nose and other suitable end mills are used to machine mold cavities, curved surfaces, and detailed profiles.
Roughing removes excess material, while finishing operations establish the required surface geometry and quality.
Mechanical Manufacturing
End milling is widely used to manufacture machine components such as mounting plates, brackets, housings, and precision fixtures.
These parts often require grooves, pockets, shoulders, and accurately machined surfaces.
Across these applications, the value of end milling lies in its ability to produce different geometric features using suitable CNC cutting tools and programmed toolpaths.
VI. Key Benefits of End Milling Operations
End milling provides several advantages for precision manufacturing.
Versatility
End mills can machine slots, pockets, shoulders, contours, and selected flat surfaces.
This makes them useful for different machining tasks on a single machine tool.
Precision and Accuracy
When combined with appropriate machine rigidity, tooling, and cutting parameters, CNC end milling can produce components with controlled dimensions and surface finish.
Wide Material Compatibility
Suitable end mills can machine aluminum, steel, stainless steel, titanium alloys, plastics, and other engineering materials.
Tool geometry, coating, and cutting conditions must be selected for the specific material.
Complex Geometry Machining
End milling supports the production of intricate features and three-dimensional surfaces, especially when used with CNC machining centers and CAM-generated toolpaths.
Flexible Production
The same CNC milling machine can often perform several different operations by changing tools and machining programs.
This flexibility is useful for custom parts, prototypes, and small-batch manufacturing.
VII. How to Use End Mills Safely and Effectively
Effective end milling depends on correct tool selection, secure setup, and appropriate cutting parameters.
The following steps provide a basic overview.
1. Check the Cutting Tool
Inspect the end mill for visible wear, chipped cutting edges, or other damage.
Confirm that its diameter, flute configuration, and material are suitable for the planned machining operation.
2. Secure the Workpiece
Use an appropriate vise, fixture, or clamping system to prevent movement during cutting.
Check that the toolpath will not interfere with clamps or other machine components.
3. Set the Cutting Parameters
Select cutting speed, feed rate, axial depth of cut, and radial engagement according to the material, cutter, and machine specifications.
Incorrect parameters can cause vibration, poor surface finish, excessive tool wear, or tool breakage.
Use the tool manufacturer's recommended starting values and adjust them according to verified machining conditions.
4. Manage Chip Evacuation
Effective chip removal prevents chips from being recut and interfering with the cutting process.
Use suitable machine chip-removal systems and follow the machine's safety procedures.
Never reach into the cutting area or manually remove chips while the cutting tool is rotating. Stop the machine as required and use appropriate chip-removal tools.
5. Choose Suitable Cooling and Lubrication
Cutting fluids, minimum quantity lubrication, or dry machining may be appropriate depending on the workpiece material, tool design, and process.
There is no single cooling method suitable for every end milling operation.
6. Verify the Machining Results
Inspect the finished feature for dimensional accuracy, surface finish, and visible defects.
If necessary, adjust machining parameters or tooling based on the measured results.
For CNC beginners, developing a consistent setup and inspection routine is essential for reliable machining.
Conclusion
End milling is a versatile machining process used to produce slots, pockets, shoulders, contours, and complex surfaces.
Understanding the differences between square, ball nose, corner radius, and roughing end mills helps operators select suitable tools for specific manufacturing tasks.
Equally important are flute count, tool material, workholding, cutting parameters, and chip evacuation.
Successful end milling depends on matching the cutting tool and machining strategy to the workpiece material, feature geometry, and required surface quality.
For manufacturers using CNC milling machines and machining centers, applying these fundamentals can improve machining consistency and reduce avoidable tool wear and production errors.
Frequently Asked Questions (FAQs)
Q1:What Is the Difference Between End Milling and Face Milling?
A:End milling commonly uses the end and peripheral cutting edges of an end mill to machine slots, pockets, shoulders, and profiles.
Face milling primarily uses a face milling cutter to machine broad flat surfaces efficiently.
Both processes can produce flat surfaces, but end milling generally offers greater flexibility for complex features, while face milling is often preferred for large, accessible planar areas.
Q2:What Are the Disadvantages of End Milling?
A:End milling requires careful selection of cutting tools, machining parameters, and workholding.
Long tool overhang, excessive cutting forces, inadequate chip evacuation, or unstable machining conditions can cause vibration, tool deflection, poor surface finish, and premature tool wear.
For large flat surfaces, a dedicated face milling cutter may also be more productive than a small end mill.
Q3:How Do I Choose the Right End Mill?
A:Start by identifying the workpiece material and the feature you need to machine.
Use square end mills for common slots and flat-bottomed pockets, ball nose end mills for curved surfaces, and suitable roughing end mills for efficient material removal.
Then select the appropriate flute count, tool material, coating, and cutting parameters according to the machining conditions and manufacturer's recommendations.
 Email
 sales1: +86 15312799623