

Energy-Saving Strategies for Horizontal Machining Centers: Optimization and Energy Recovery
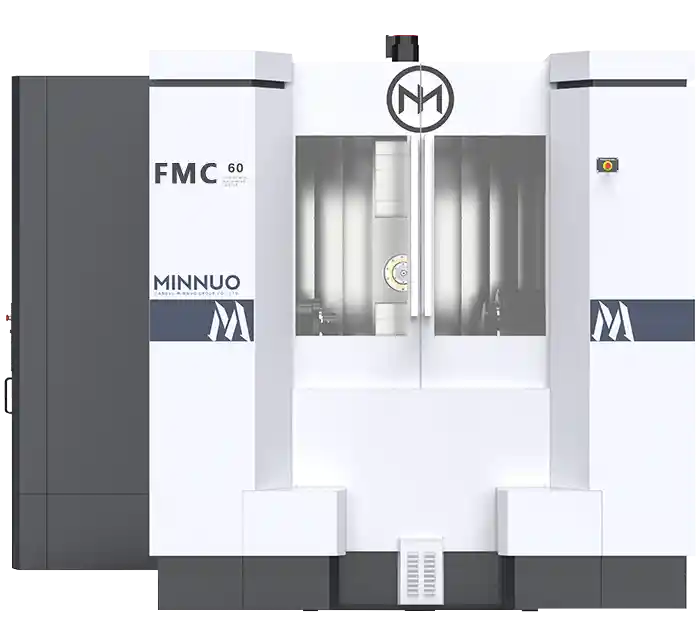
Energy consumption is an important operating cost for horizontal machining centers (HMCs), especially in workshops running multiple machines over extended production shifts. Electricity is consumed not only during cutting but also by spindle drives, hydraulic systems, coolant pumps, chip conveyors, and other auxiliary equipment.
The two main approaches to improving energy efficiency in horizontal machining centers are dynamic energy optimization and energy recovery. Dynamic optimization reduces unnecessary power consumption through improved machining parameters, standby management, and auxiliary system control. Energy recovery can reuse certain forms of otherwise wasted energy, provided the machine and operating conditions support it.
However, energy savings depend on the machine configuration, machining cycle, production schedule, and electrical system. No single strategy guarantees the same results for every workshop.
This guide explains where horizontal machining centers consume energy, how to optimize their operation, when energy recovery is practical, and how to calculate potential electricity savings and return on investment.
1. Where Do Horizontal Machining Centers Consume Energy?
Before implementing energy-saving measures, manufacturers should identify which machine components consume electricity and when that consumption occurs.
A horizontal machining center typically includes several electrical systems with different operating characteristics.
| Energy-Consuming System | Typical Function | Potential Energy-Saving Opportunity |
|---|---|---|
| Spindle drive | Rotates the cutting tool | Optimize cutting conditions and cycle time |
| Feed-axis drives | Move machine axes | Reduce unnecessary movement and idle time |
| Hydraulic system | Operates clamping or other mechanisms | Demand-based operation where supported |
| Coolant system | Supplies cutting fluid | Optimize pump operation and fluid delivery |
| Spindle chiller | Controls spindle temperature | Improve thermal management efficiency |
| Chip conveyor | Removes machining chips | Use appropriate intermittent operation |
| CNC and auxiliary equipment | Controls and supports machine operation | Manage standby consumption |
| Tool and pallet changers | Automate production | Reduce unnecessary waiting and non-cutting time |
The largest energy consumer is not necessarily the spindle.
During heavy cutting, spindle power demand may dominate. However, during setup, waiting, and light machining, auxiliary systems can account for a substantial portion of total electricity consumption.
1.1 Standby Energy Consumption
Horizontal machining centers may remain powered on during tool preparation, workpiece inspection, lunch breaks, or production delays.
Even when the spindle is not cutting, equipment such as hydraulic pumps, control systems, cooling units, and other auxiliaries may continue operating.
This creates opportunities for reducing energy consumption during nonproductive periods.
The first step is to measure actual standby power rather than assume that every machine consumes the same amount.
1.2 Inefficient Machining Parameters
Cutting speed, feed rate, depth of cut, and tool selection affect both machining time and electrical consumption.
Using the same cutting parameters for different materials or machining operations can result in inefficient cutting conditions.
For example, a machine may consume relatively little instantaneous spindle power during a light cut but require a longer machining cycle.
In this situation, total energy consumption per workpiece may be higher because auxiliary systems continue consuming electricity throughout the extended cycle.
1.3 Unused Braking Energy and Waste Heat
During spindle deceleration or feed-axis braking, some electrical drive systems can convert mechanical energy back into electrical energy.
Without suitable recovery equipment, the energy may be dissipated through braking resistors.
Horizontal machining centers also generate heat through motors, hydraulic systems, coolant circulation, and other components.
Some of this thermal energy may be recoverable, although its practical value depends on temperature, operating duration, and whether the facility has a suitable use for the recovered heat.
2. Dynamic Energy Efficiency Optimization
Dynamic energy optimization focuses on reducing unnecessary energy consumption while maintaining acceptable machining productivity, accuracy, and reliability.
The most practical strategies include optimizing cutting parameters, managing standby conditions, and controlling auxiliary equipment according to actual demand.
2.1 Optimize Cutting Parameters for Energy per Part
The objective of energy-efficient machining is not simply to minimize spindle power at every moment.
Instead, manufacturers should evaluate how much electricity is required to produce an acceptable finished component.
Energy Consumption per Part (kWh/part) = Total Energy Consumed (kWh) ÷ Number of Accepted Parts
This indicator considers the relationship between machining efficiency and energy use.
For example, increasing material removal rate within the allowable machining conditions may reduce cycle time and the energy consumed by auxiliary systems.
However, excessively aggressive parameters may increase tool wear, vibration, cutting forces, or scrap rates.
Therefore, energy optimization should consider:
- Workpiece material and hardness
- Cutting tool geometry and coating
- Cutting speed and feed rate
- Depth and width of cut
- Spindle power and torque requirements
- Tool life and surface quality
- Total machining cycle time
Practical Optimization Method
Step 1: Record the current machining cycle time, power consumption, and part quality.
Step 2: Identify operations with unnecessary air cutting, excessive cycle time, or inefficient tool engagement.
Step 3: Adjust cutting parameters within the tool manufacturer's recommended operating range.
Step 4: Compare energy consumption per accepted part before and after optimization.
Step 5: Verify dimensional accuracy, surface finish, tool life, and machine stability.
A higher spindle load percentage does not automatically mean better energy efficiency. The appropriate operating range depends on the machine, cutting process, and production requirements.
2.2 Reduce Standby Power Consumption
Standby management can be an effective energy-saving strategy for horizontal machining centers with frequent production interruptions.
Some CNC systems support energy-saving modes or PLC-controlled auxiliary shutdown functions.
Depending on the equipment, these functions may allow certain nonessential systems to enter a reduced-power state after a defined period of inactivity.
Recommended Measures:
- Identify predictable idle periods in the production schedule.
- Enable manufacturer-supported standby functions where available.
- Reduce unnecessary operation of suitable auxiliary equipment.
- Avoid leaving machines fully powered during extended, nonproductive periods when safe shutdown is permitted.
- Verify the restart procedure before returning to production.
Standby management must account for equipment safety and thermal stability.
For example, stopping spindle cooling or hydraulic circulation without evaluating the consequences may affect machine temperature, clamping functions, or readiness for machining.
Automatic shutdown logic should be implemented only through approved machine control functions and validated by qualified personnel.
2.3 Optimize Auxiliary System Operation
Auxiliary equipment can consume electricity during both cutting and non-cutting periods.
Improving auxiliary system control may therefore reduce energy consumption without necessarily changing the cutting process.
Coolant Pump Optimization
Coolant pumps should provide the flow and pressure required for the specific machining operation.
Potential measures include:
- Selecting appropriate pump capacity
- Improving nozzle positioning
- Maintaining filters and coolant delivery lines
- Using demand-based pump operation when supported
- Evaluating variable-speed pumps for suitable applications
Variable-frequency control can reduce pump energy use in appropriate systems, but savings depend on pump characteristics and hydraulic operating requirements.
Reducing pump speed should never compromise cooling, lubrication, chip removal, or tool life.
Chip Conveyor Optimization
Chip conveyors do not always need to operate continuously.
Where supported by the machine design, intermittent conveyor operation may reduce unnecessary running time.
The operating schedule must still provide reliable chip removal and prevent chip accumulation.
Hydraulic and Cooling Systems
Hydraulic pumps and cooling units may also offer energy-saving opportunities through demand-based operation or more efficient component selection.
However, critical functions such as hydraulic clamping and spindle temperature control must be maintained according to machine requirements.
The goal is to reduce unnecessary auxiliary energy consumption without compromising machining safety, quality, or thermal stability.
3. Energy Recovery Technologies for Horizontal Machining Centers
Energy recovery provides another approach to improving machine tool energy efficiency.
Unlike operational optimization, energy recovery requires suitable electrical or thermal equipment to capture and reuse energy that would otherwise be wasted.
Two possible approaches are regenerative braking and waste heat recovery.
3.1 Regenerative Braking Energy Recovery
When a motor decelerates, it may operate as a generator and convert part of the mechanical energy into electrical energy.
In a conventional non-regenerative drive system, braking energy may be dissipated as heat through braking resistors.
A compatible regenerative drive system can instead make some of this energy available for reuse.
Depending on the drive architecture, recovered electrical energy may be:
- Shared through a common DC link with other compatible drives.
- Returned to the electrical supply through a suitable regenerative power module.
This technology is most relevant when machining operations involve repeated acceleration and deceleration.
Suitable Operating Conditions
Regenerative braking may be worth evaluating in machining processes involving:
- Frequent spindle speed changes
- Repeated spindle acceleration and deceleration
- Frequent tool changes requiring spindle stopping
- Repeated feed-axis acceleration and braking
The potential savings depend on the moving inertia, speed profile, frequency of deceleration, drive efficiency, and electrical architecture.
Important Technical Considerations
Before selecting a regenerative system, verify:
- Whether the machine already uses a regenerative drive.
- Whether the drive and DC link support energy sharing or recovery.
- Whether the electrical supply can accept returned energy.
- The amount of recoverable braking energy during actual production.
- The additional losses and operating costs of the recovery system.
Regenerative systems also have their own electrical losses. Where braking events are infrequent, the additional equipment may provide limited net benefit.
Retrofitting regenerative drives requires electrical compatibility and safety evaluation by qualified personnel. Emergency-stop functions must never be modified merely to increase energy recovery.
3.2 Waste Heat Recovery
Horizontal machining centers generate waste heat through spindle motors, hydraulic systems, coolant circulation, and other equipment.
In some installations, this heat may be transferred through a heat exchanger and used for suitable facility heating or process applications.
Possible heat sources include:
- Hydraulic oil cooling circuits
- Coolant temperature-control systems
- Spindle cooling systems
- Other compatible industrial cooling circuits
The feasibility of waste heat recovery depends on the available heat quantity and temperature, operating duration, and the heating requirements of the facility.
For example, a workshop with continuous machine operation and a compatible heating demand may be able to evaluate heat recovery from a central cooling system.
However, this does not mean every machining center can economically recover useful heat.
Waste Heat Recovery Limitations
- Recovered heat may be too low in temperature for direct use.
- Heating demand may vary seasonally.
- Heat exchangers, pumps, and controls introduce additional costs and energy consumption.
- Changes to machine cooling circuits must not compromise thermal stability.
- Heat recovery may be more practical at workshop level than through individual machine retrofits.
For these reasons, waste heat recovery should generally be treated as a project-specific engineering option rather than a standard energy-saving feature of every horizontal machining center.
3.3 Comparing Energy Recovery Options
| Recovery Technology | Primary Energy Source | Suitable Conditions | Main Considerations |
|---|---|---|---|
| Regenerative braking | Electrical energy generated during drive deceleration | Frequent acceleration and braking | Drive compatibility, regeneration losses, braking frequency |
| Waste heat recovery | Heat from suitable machine cooling circuits | Continuous operation and usable heat demand | Heat temperature, thermal demand, integration cost |
Selection Recommendation: Evaluate actual recoverable energy before purchasing additional equipment. A technically feasible recovery system is not necessarily an economically worthwhile retrofit.
4. How to Measure Energy Savings and Return on Investment
Reliable energy-saving decisions require measured baseline data and consistent comparison conditions.
Manufacturers should avoid relying only on motor rated power, theoretical efficiency percentages, or generalized industry estimates.
4.1 Establish an Energy Consumption Baseline
Record machine electricity consumption under representative operating conditions.
Useful operating states include:
- Powered-on standby
- Setup and tool preparation
- Rough machining
- Finish machining
- Tool changes and positioning movements
- Production interruptions
Measurements should include the relevant machine electrical systems and clearly define whether external equipment, such as centralized compressors or cooling systems, is included.
Energy monitoring should also record the number of acceptable workpieces produced.
For consistent comparison, use similar workpieces, materials, machining programs, production volumes, and quality requirements.
The ISO 14955-2 standard provides measurement methods for energy supplied to machine tools and their components under specified conditions.
4.2 Calculate Annual Electricity Savings
A basic calculation is:
Annual Energy Savings (kWh) = Annual Baseline Electricity Consumption − Annual Electricity Consumption After Optimization
For a specific standby-power improvement:
Annual Standby Energy Savings (kWh) = Power Reduction (kW) × Eligible Idle Hours per Day × Operating Days per Year
To calculate electricity cost savings:
Annual Electricity Cost Savings = Annual Energy Savings (kWh) × Electricity Price per kWh
These formulas provide estimates based on the stated operating conditions.
Actual savings must be verified using measured electricity consumption.
4.3 Evaluate Energy Consumption per Part
Lower total electricity consumption does not always mean that a machining process is more efficient.
For example, a factory may consume less electricity simply because it produces fewer components.
Therefore, evaluate:
Energy per Accepted Part (kWh/part) = Total Electricity Consumption (kWh) ÷ Number of Accepted Parts
This metric helps determine whether energy efficiency has improved under comparable production conditions.
It is particularly useful when assessing cutting parameter changes, cycle time improvements, and auxiliary system optimization.
4.4 Calculate Simple Payback Period
For equipment retrofits, the investment decision should consider installation cost, operating expenses, and expected annual savings.
Simple Payback Period (Years) = Initial Investment ÷ Annual Net Cost Savings
Annual net savings should account for relevant additional maintenance and operating costs.
A more complete economic assessment may also include equipment lifetime, downtime during installation, replacement costs, and changes in production performance.
4.5 Estimating Environmental Benefits
Reducing electricity consumption can also lower indirect greenhouse gas emissions associated with purchased electricity.
A simplified estimate is:
Estimated Emissions Reduction (kg CO₂e) = Electricity Savings (kWh) × Applicable Electricity Emission Factor (kg CO₂e/kWh)
The emission factor must correspond to the relevant electricity supply, location, reporting period, and accounting method.
This calculation does not represent a complete product carbon footprint or automatically establish regulatory compliance.
5. Practical Example: Energy Savings for 10 Horizontal Machining Centers
The following example demonstrates how a workshop can estimate the potential benefit of reducing standby power.
This is an illustrative calculation using assumed operating data, not a verified MINNUO customer project or guaranteed equipment performance result.
5.1 Initial Operating Conditions
Assume a workshop operates 10 horizontal machining centers.
Each machine has:
| Parameter | Assumed Value |
|---|---|
| Number of machines | 10 |
| Average standby power before optimization | 5 kW |
| Average reduced-power standby consumption | 2 kW |
| Eligible idle time | 6 hours per day |
| Operating days | 250 days per year |
| Electricity price | RMB 1.20/kWh |
The assumed standby-power reduction is:
Power Reduction = 5 − 2 = 3 kW
5.2 Annual Energy-Saving Calculation
Annual Savings per Machine
Annual Energy Savings = 3 × 6 × 250
Annual Energy Savings = 4,500 kWh
Annual Savings for 10 Machines
Total Annual Energy Savings = 4,500 × 10
Total Annual Energy Savings = 45,000 kWh
Annual Electricity Cost Savings
Annual Cost Savings = 45,000 × 1.20
Annual Electricity Cost Savings = RMB 54,000
Under these assumptions, the workshop could theoretically reduce annual electricity consumption by 45,000 kWh through standby-power optimization alone.
5.3 Important Limitations
The calculation assumes that:
- Each machine has six eligible idle hours per operating day.
- The average reduction from 5 kW to 2 kW is achieved throughout those eligible periods.
- Energy-saving settings do not create additional scrap, delays, or production losses.
- The electricity tariff remains constant.
Actual savings may be lower if the machines have shorter idle periods, require continuous temperature control, or cannot enter the assumed reduced-power state.
Additional savings from cutting optimization or energy recovery should be calculated separately and checked for overlap.
The key lesson is that measurable operational improvements can provide a useful starting point before investing in more complex energy recovery technologies.
6. Common Energy-Saving Mistakes to Avoid
6.1 Focusing Only on Equipment Upgrades
Installing a more efficient component does not guarantee that the complete machining process will consume less energy.
Unnecessary waiting time, inefficient cutting parameters, and continuously operating auxiliaries may continue to waste electricity.
Better Approach: Measure energy consumption first, improve operational efficiency, and then evaluate hardware upgrades where necessary.
6.2 Assuming Higher Spindle Load Always Means Higher Efficiency
Increasing spindle load may shorten machining time in some applications, but it may also increase tool wear or compromise machining quality.
Better Approach: Compare energy per accepted part while maintaining tool life and workpiece specifications.
6.3 Switching Off Every Auxiliary System
Turning off cooling, hydraulic, or other support systems without considering the consequences may affect thermal stability, machine readiness, or safety.
Better Approach: Use manufacturer-approved energy management functions and validate the resulting machine behavior.
6.4 Overestimating Energy Recovery Benefits
A regenerative module cannot recover more energy than the suitable braking events make available.
Likewise, waste heat recovery requires both a suitable heat source and a practical use for the recovered heat.
Better Approach: Estimate recoverable energy from actual machine operation, then compare expected net savings with equipment and maintenance costs.
6.5 Using Unverified Energy-Saving Percentages
Fixed claims such as a universal 30% or 40% electricity reduction may not apply to another machine or machining process.
Better Approach: Use transparent measurement methods, document operating conditions, and distinguish calculated estimates from verified results.
7. Frequently Asked Questions (FAQ)
Q1. How can I reduce the electricity consumption of a horizontal machining center?
A:Start by measuring electricity consumption during cutting, standby, setup, and other operating states.
Then optimize machining parameters, reduce unnecessary idle time, and improve auxiliary system control. Evaluate energy recovery only when the machine configuration and operating conditions justify it.
Q2. Which components consume the most electricity in a horizontal machining center?
A:The main consumers can include spindle drives, hydraulic systems, coolant pumps, spindle chillers, and other auxiliary equipment.
Their relative contributions depend on the machining process and machine operating state.
Q3. Can regenerative braking reduce CNC machine energy consumption?
A:Yes, a compatible regenerative drive can recover some braking energy during suitable deceleration events.
However, net savings depend on the frequency of braking, recoverable energy, drive architecture, and system losses.
Q4. Is waste heat recovery practical for all horizontal machining centers?
A:No. Waste heat recovery requires a suitable heat source, adequate thermal output, and a practical use for the recovered heat.
It may be more suitable for selected installations or centralized workshop cooling systems than for every individual machine.
Q5. How should manufacturers measure CNC machine energy efficiency?
A:Measure energy consumption under representative operating conditions and calculate electricity use per accepted workpiece.
Compare results using consistent production and quality requirements.
Q6. What is the best first step for a low-budget energy-saving project?
A:Begin with energy monitoring, standby management, reduction of nonproductive time, and process optimization.
These measures can often be evaluated before investing in additional energy recovery hardware.
Conclusion
Improving the energy efficiency of horizontal machining centers requires a combination of operational optimization and appropriate technology.
Dynamic energy efficiency optimization should generally be the starting point. Improving cutting efficiency, reducing unnecessary standby consumption, and managing auxiliary equipment according to actual demand can help lower electricity use.
Energy recovery provides additional opportunities where technically and economically feasible. Regenerative braking can recover energy from suitable drive deceleration events, while waste heat recovery may be practical in selected installations.
However, the effectiveness of these measures depends on the machine configuration, production cycle, energy consumption profile, and system compatibility.
For manufacturers planning an energy-saving improvement project, a practical approach is to:
- Measure the machine's current energy consumption.
- Identify unnecessary standby and auxiliary power use.
- Optimize machining processes without compromising quality.
- Evaluate energy recovery based on actual operating data.
- Verify electricity savings and calculate return on investment.
For more information about CNC machining equipment and suitable machine configurations, contact MINNUO to discuss your production requirements.
The most effective energy-saving strategy is one that reduces electricity consumption per acceptable workpiece while maintaining machining accuracy, productivity, and reliability.
 Email
 sales1: +86 15312799623