

Slant Bed CNC Lathe Machine Buying Guide: 4 Specs That Matter Most
When selecting a slant bed CNC lathe machine, focus on four systems first: spindle performance, turret capability, guideway and machine structure, and CNC control. Maximum rpm, motor power, chuck size, or turret station count alone cannot determine whether a machine fits your production. The right configuration depends on workpiece diameter, material, tolerance, machining operations, batch size, and target cycle time.
What Should Buyers Compare on a Slant Bed CNC Lathe Machine?
For most industrial turning applications, procurement engineers should evaluate four areas:
- Spindle performance — maximum rpm, torque curve, continuous power, spindle nose, bore, chuck size, and usable bar capacity.
- Turret capability — number of stations, BMT/VDI interface, live-tool speed and torque, Y-axis travel, and C-axis functions.
- Guideway and machine structure — rigidity, damping, rapid traverse, thermal behavior, and axis stability.
- CNC control — controlled axes and paths, spindle synchronization, programming, automation interfaces, diagnostics, and service support.
The core rule is simple:
Select the machine around the part and machining process—not around the largest number on the specification sheet.
Why Slant Bed CNC Lathe Specifications Are Often Misread
Maximum RPM Does Not Equal Cutting Capability
A 5,000 rpm spindle is not automatically better than a 4,000 rpm spindle.
High maximum spindle speed becomes important when small-diameter parts require high rotational speed to maintain the recommended cutting speed.
For large-diameter turning, heavy steel roughing, interrupted cutting, threading, and difficult-to-machine alloys, more important questions may be:
- How much torque is available at the actual cutting speed?
- How much spindle power is available continuously?
- Is the spindle and workholding system rigid enough?
- Can the machine maintain dimensional stability over a long production cycle?
DN Solutions currently lists the PUMA 2600SY II with 4,000 r/min maximum spindle speed, 22 kW maximum spindle power, and 599 N·m maximum spindle torque. It also publishes 260/105/830 mm X/Y/Z travel, 12 turret stations, and 5,000 r/min rotary tooling. The manufacturer also notes that specifications may vary by region. DN Solutions PUMA 2600SY II official specifications
These maximum values should not be interpreted as occurring simultaneously.
Maximum Power, Torque, and RPM Usually Occur at Different Operating Points
This is one of the most important concepts in spindle comparison.
Maximum rpm, maximum torque, and maximum motor power normally describe different sections of the spindle characteristic curve.
For an accurate comparison, request the manufacturer's spindle power/torque curve.
1. Spindle Specs: RPM, Torque, Power, Bore, and Bar Capacity
For most procurement projects, evaluate spindle specifications approximately in this order:
usable bar capacity → spindle nose → chuck size → torque curve → continuous power → short-time power → maximum rpm
How to Calculate Spindle Torque
For mechanical spindle power at a known operating speed:
T = (9550 × P) ÷ n
Where:
- T = spindle torque, N·m
- P = mechanical spindle power at that operating point, kW
- n = spindle speed at the same operating point, rpm
The key condition is:
Power and spindle speed must refer to the same operating point.
Example
If a spindle mechanically delivers:
P = 22 kW
at:
n = 4,000 rpm
then:
T = (9550 × 22) ÷ 4,000
T ≈ 52.5 N·m
This does not contradict a manufacturer's published maximum torque such as 599 N·m, because maximum torque generally occurs at a much lower spindle speed.
For purchasing decisions, use the OEM torque/power curve whenever available rather than calculating performance from isolated maximum values.
How to Calculate the Spindle Speed Your Part Requires
For metric turning:
n = (1000 × Vc) ÷ (π × Dm)
Where:
- n = spindle speed, rpm
- Vc = cutting speed, m/min
- Dm = effective machining diameter, mm
- π ≈ 3.1416
Example: Ø50 mm Workpiece
Assume:
Vc = 200 m/min
Dm = 50 mm
Then:
n = (1000 × 200) ÷ (3.1416 × 50)
n ≈ 1,273 rpm
Both a 4,000 rpm and a 5,000 rpm spindle provide more than enough speed capacity for this operation.
Example: Ø15 mm Workpiece
Using the same cutting speed:
n = (1000 × 200) ÷ (3.1416 × 15)
n ≈ 4,244 rpm
Now the difference matters.
A spindle limited to 4,000 rpm cannot fully achieve a cutting speed of 200 m/min at Ø15 mm, whereas a 5,000 rpm spindle can.
Therefore:
Maximum spindle speed should always be evaluated against workpiece diameter and required cutting speed.
Continuous Power Can Matter More Than Peak Power
Spindle power may be published as:
- maximum power;
- 20-minute or 30-minute rating;
- percentage duty such as 40% ED;
- continuous power.
These values are not equivalent.
For the current Japanese QUICK TURN 200MSY (500U), Mazak publishes:
- maximum spindle speed: 5,000 min⁻¹
- maximum torque: 140 N·m at 40% ED
- spindle motor: 15 kW at 40% ED
- continuous spindle motor rating: 11 kW.
For sustained roughing, the continuous rating may be more meaningful than the highest short-duration kW value.
Spindle Bore and Bar Capacity Are Different Specifications
A common procurement mistake is treating spindle bore and usable bar capacity as the same value.
They are not.
Actual usable bar diameter may be restricted by:
- drawtube;
- chuck;
- collet;
- spindle liner;
- bar-feeder interface.
The Haas ST-20Y provides a clear example:
- spindle nose: A2-6
- maximum rating: 14.9 kW
- maximum speed: 4,000 rpm
- maximum torque: 203 N·m at 500 rpm
- spindle bore: 88.9 mm
- bar capacity: 64 mm.Haas ST-20Y official specifications
For bar-fed production, specify:
maximum usable bar diameter through the complete installed spindle and workholding system
rather than spindle bore alone.
2. Turret Specs: Stations, Live Tooling, BMT/VDI, Y-Axis, and C-Axis
A “12-station turret” is not a complete technical specification.
Two machines can both have 12 stations and still offer substantially different machining capability.
| Turret Parameter | What to Compare | Why It Matters |
|---|---|---|
| Tool interface | BMT / VDI / proprietary | Holder compatibility and rigidity |
| Number of stations | 10 / 12 / 16 etc. | Tools available without changeover |
| Live-tool speed | rpm | Drilling and milling speed range |
| Live-tool torque | N·m | Tapping and larger cutter capability |
| Live-tool power | kW | Material-removal capability |
| Y-axis travel | mm | Off-center machining range |
| C-axis functions | Positioning / interpolation | Flats, cross holes, angular features |
| Turret index time | s | Short-cycle productivity |
| Positioning repeatability | μm or mm | Tool-position consistency |
Mazak's current QUICK TURN 200MSY specification combines 12 tool positions with:
- maximum live-tool speed: 5,000 min⁻¹
- maximum live-tool torque: 47 N·m at 40% ED
- live-tool motor: 5.5 kW at 40% ED
- continuous live-tool motor rating: 3.7 kW.
DN Solutions' PUMA 2600SY II also publishes:
- 12 stations
- 5,000 r/min rotary tooling
- 105 mm Y-axis travel.
Both are “12-station” machines, yet station count alone does not define their turn-mill capability.
BMT vs VDI: Which Is Better?
There is no universal winner.
Instead, compare:
- coupling geometry;
- clamping structure;
- holder dimensions;
- tool overhang;
- live-tool torque;
- live-tool speed;
- bearing arrangement;
- tooling availability.
For heavy driven-tool cutting, turret rigidity and holder overhang may matter more than the interface name itself.
For factories with an established tooling system, compatibility and replacement-tool availability also affect lifecycle cost.
3. Guideway and Machine Structure: What Determines Rigidity and Stability?
The common statement:
Box ways are rigid; linear guides are fast.
is too simplistic for a procurement decision.
Guideway performance depends on the complete mechanical structure.
Important factors include:
- machine mass;
- bed geometry;
- saddle structure;
- guideway dimensions and spacing;
- preload;
- ballscrew design;
- servo thrust;
- rapid traverse;
- acceleration;
- lubrication;
- vibration damping;
- thermal behavior.
When Heavy-Cutting Capability Matters
For heavy steel roughing and interrupted cutting, buyers should pay particular attention to:
- spindle torque at low and medium speed;
- machine structural mass;
- guideway spacing;
- workholding rigidity;
- damping;
- continuous spindle power.
When Speed and Non-Cutting Time Matter
For small components and high-volume production, other parameters can become more important:
- rapid traverse;
- axis acceleration;
- turret indexing speed;
- spindle acceleration/deceleration;
- tool-change strategy.
The correct question is:
Can the complete machine structure maintain the required accuracy, surface finish, and stability under the actual production cycle?
The guideway label alone cannot answer that question.
4. CNC Control: Match the Control to the Machine Architecture
A simple turning center may only require:
- X axis;
- Z axis;
- main spindle.
A more advanced slant bed CNC lathe may include:
- Y axis;
- C axis;
- live tooling;
- sub-spindle;
- multiple tool carriers;
- bar feeder;
- robot automation.
As machine complexity increases, CNC architecture becomes more important.
Do not ask only:
Which CNC brand does the machine use?
Ask:
Can this exact control configuration execute, synchronize, diagnose, and support the process required by our parts?
| CNC Item | Procurement Question |
|---|---|
| Control generation | Is the platform currently supported? |
| Controlled axes | Does it support every installed axis? |
| Controlled paths | Can multiple tool carriers or spindles operate as required? |
| Y/C-axis functions | Are the required functions installed? |
| Spindle synchronization | Can main/sub-spindle transfer be synchronized? |
| Tool management | Does it support the required tool-life strategy? |
| CAM compatibility | Is a proven postprocessor available? |
| PLC/ladder support | Can service engineers diagnose machine logic? |
| Connectivity | Can the machine exchange required production data? |
| Automation interface | Can robots or bar feeders be integrated? |
| Regional support | Is qualified technical support available? |
For a simple shaft-turning process, paying for complex multitasking functions may not create value.
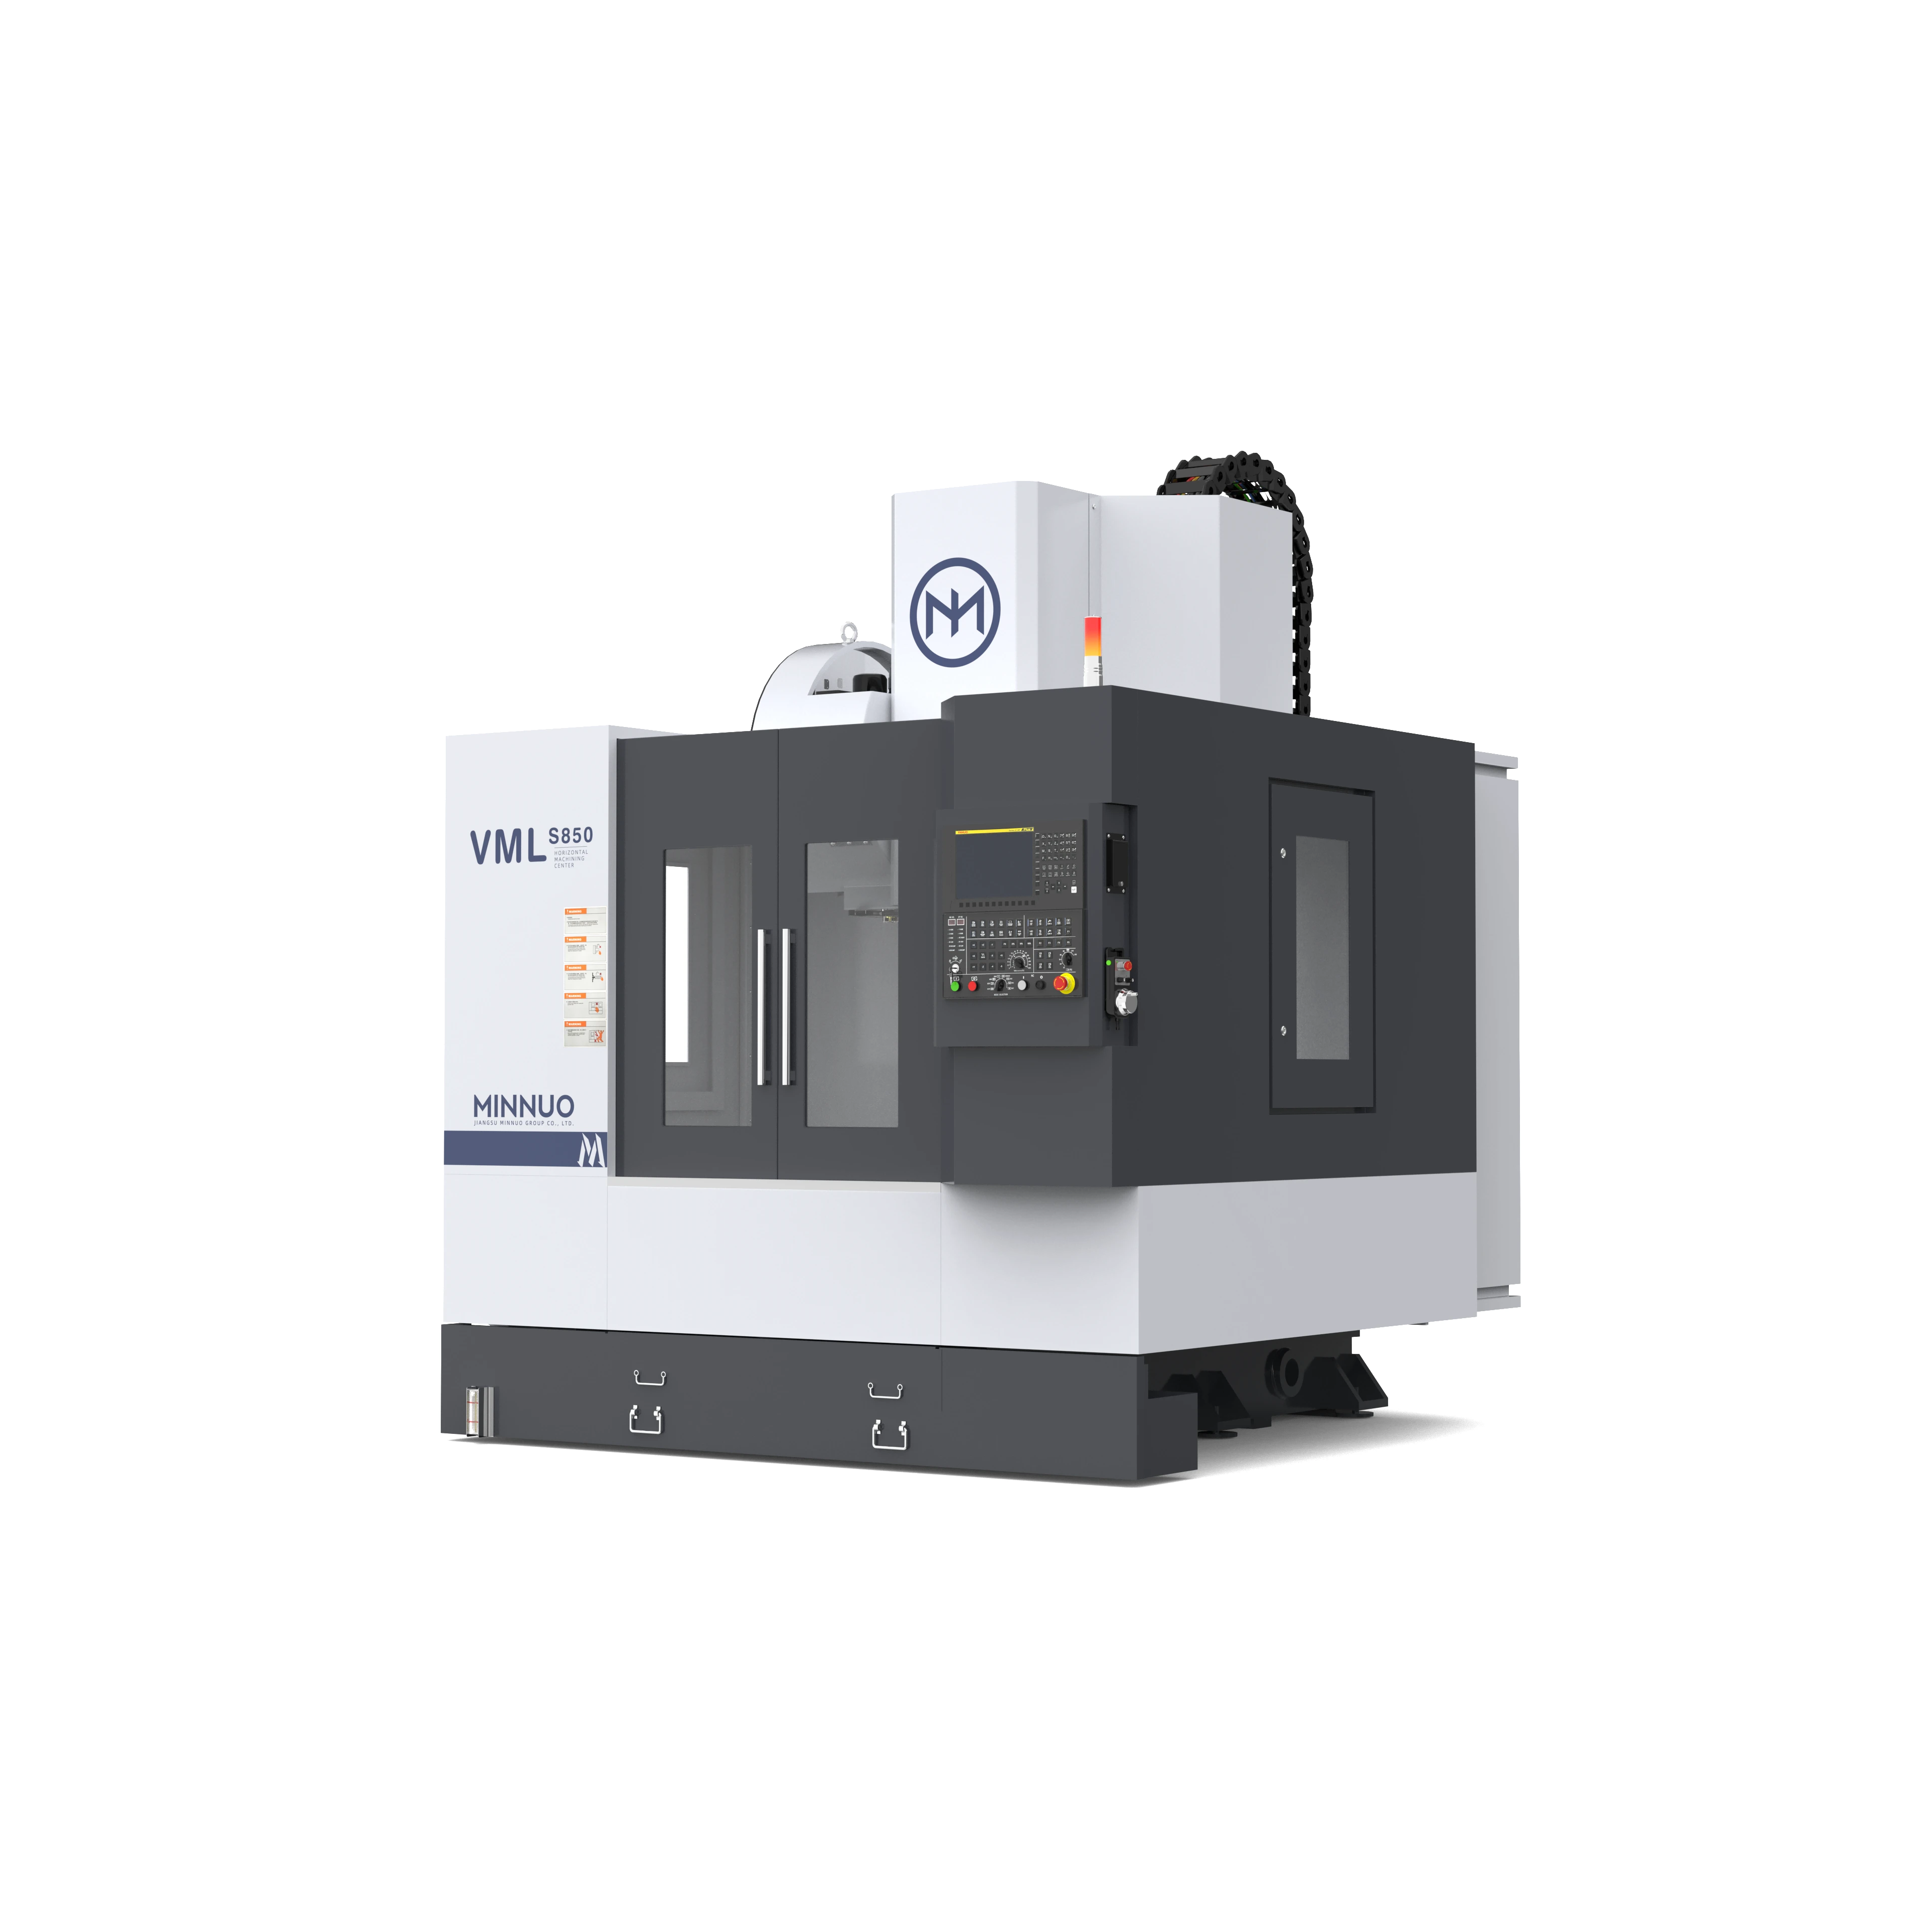
For a component requiring turning, cross drilling, flats, radial holes, and back-side machining, Y-axis, live tooling, and a sub-spindle may eliminate multiple secondary operations.
Which Slant Bed CNC Lathe Configuration Fits Your Application?
| Application | Specifications to Prioritize |
|---|---|
| Heavy steel roughing | Low-speed torque + continuous power + structural rigidity |
| Small-diameter high-speed turning | Maximum rpm + acceleration + thermal stability |
| Bar-fed shaft production | Usable bar capacity + spindle nose + feeder compatibility |
| Turn-mill components | Live-tool torque + Y axis + C-axis interpolation |
| Short-cycle mass production | Turret index time + rapid traverse + acceleration |
| Precision components | Thermal stability + positioning/repeatability + test-cut results |
| Large-diameter machining | Chuck/spindle capacity + low-speed torque + machine structure |
| Automated production | CNC connectivity + automation interface + process monitoring |
This application-based approach is more useful than trying to identify one universally “best” machine.
How to Verify CNC Lathe Accuracy Before Acceptance
A catalogue tells you what the machine is designed to achieve.
A Factory Acceptance Test (FAT) should confirm whether the supplied machine meets the agreed technical requirements.
Positioning Accuracy and Repeatability
ISO 230-2:2014 specifies methods for testing and evaluating the positioning accuracy and repeatability of numerically controlled machine-tool axes by direct measurement. It applies to linear and rotary axes and may be used for acceptance testing, comparison testing, periodic verification, and machine compensation. ISO reviewed and confirmed the edition in 2025. ISO 230-2:2014 official standard page
Geometric Tests for CNC Turning Machines
ISO 13041-1:2020 specifies geometric tests and applicable tolerances for normal-accuracy CNC turning machines and turning centres with horizontal workholding spindle(s). ISO reviewed and confirmed this edition in 2025.ISO 13041-1:2020 official standard page
A practical FAT may include:
| Test Item | Evidence to Record | Typical Unit |
|---|---|---|
| X/Z positioning | Bidirectional positioning results | μm or mm |
| X/Z repeatability | Repeated positioning data | μm or mm |
| Spindle runout | Indicator measurement | μm or mm |
| Thermal displacement | Change vs time/temperature | μm |
| Turret positioning | Repeated indexing result | μm or mm |
| C-axis | Positioning/interpolation result | ° or arc-sec |
| Live tooling | Speed and loaded cutting test | rpm / kW |
| Test component | Diameter, roundness, cylindricity | μm or mm |
Why Measurement Resolution Is Not Machine Accuracy
A laser interferometer is one established method for machine-axis verification.
Renishaw currently publishes the XL-80 with:
- 1 nm linear resolution
- maximum linear measurement speed: 4 m/s
- sampling up to 50 kHz
- linear measurement accuracy: ±0.5 ppm under the stated environmental conditions.
However:
Measurement-system resolution is not the same as machine-tool accuracy.
A measuring instrument capable of resolving 1 nm does not mean that the CNC lathe should position within 1 nm.
Machine acceptance limits must be defined separately from the instrument's measurement capability.
How Machine Configuration Can Reduce Cycle Time
Additional machine functions only create value when they remove real production steps.
Consider a component that requires:
- OD turning;
- facing;
- axial drilling;
- cross drilling;
- flat milling;
- back-side machining.
A basic two-axis lathe may require several setups or transfer to another machine.
A Y-axis turn-mill machine with live tooling and a sub-spindle may complete more of these operations in one setup.
The relevant procurement question is:
How much setup, handling, secondary machining, and cycle time can the additional machine capability eliminate?
Cycle-Time Reduction Formula
Cycle-Time Reduction (%) = [(told − tnew) ÷ told] × 100%
Where:
- told = original cycle time
- tnew = new cycle time
Example:
If the process changes from:
103 s → 34 s
then:
[(103 − 34) ÷ 103] × 100%
≈ 67% cycle-time reduction
This does not mean that adding a Y axis, second turret, or sub-spindle automatically creates a 67% improvement.
Actual results depend on:
- part geometry;
- simultaneous machining opportunities;
- tooling;
- workholding;
- programming;
- loading;
- process balance.
The purchasing lesson is:
Do not buy additional axes because the specification sheet looks more advanced. Buy them when they eliminate measurable setups or production bottlenecks.
Slant Bed CNC Lathe Machine FAQ
Q: Is higher maximum spindle speed always better?
A: No. Required rpm depends on cutting speed and workpiece diameter.
Use:
n = (1000 × Vc) ÷ (π × Dm)
Then compare the available torque and continuous power at the required operating speed.
Q: If a CNC lathe lists 22 kW, 599 N·m, and 4,000 rpm, are all three available simultaneously?
A: Usually not. Maximum torque, maximum power, and maximum spindle speed generally occur at different points on the spindle characteristic curve. Request the OEM torque/power curve.
Q: Are spindle bore and usable bar capacity the same?
A: No. Spindle bore is a physical spindle dimension. Usable bar capacity may be further restricted by the drawtube, chuck, collet, liner, and bar-feeder configuration.
Q: Which turret interface is better?
A: There is no universal winner. Compare turret rigidity, holder dimensions, tool overhang, driven-tool torque, driven-tool speed, bearing arrangement, and tooling availability.
Q: Which guideway design should I choose?
A: It depends on the production requirement. Heavy roughing may prioritize damping and structural rigidity, while high-volume production may prioritize rapid traverse and acceleration. Evaluate the complete machine structure.
Q: What should procurement engineers verify before acceptance?
A: Typical items include X/Z positioning and repeatability, spindle runout, thermal behavior, turret positioning, applicable Y/C-axis tests, live-tool operation, and representative test cutting. ISO 230-2 provides a recognized framework for positioning and repeatability testing.
Q: When should I choose a Y-axis configuration?
A: It becomes valuable when off-center drilling, milling, flats, cross holes, or other secondary operations can be completed in the same setup, reducing transfers and cycle time.
Quick Procurement Checklist
Before issuing a purchase order, confirm:
- maximum part diameter and length;
- material range;
- required cutting speed;
- heavy-roughing requirement;
- usable bar diameter;
- spindle nose and chuck size;
- spindle torque/power curve;
- continuous spindle power;
- turret interface and station count;
- live-tool torque, power, and rpm;
- Y-axis travel;
- C-axis requirements;
- guideway and structural design;
- positioning and repeatability requirements;
- CNC control configuration;
- CAM/postprocessor compatibility;
- bar-feeder or robot interface;
- FAT method and acceptance limits;
- regional technical support.
 Email
 sales1: +86 15312799623